

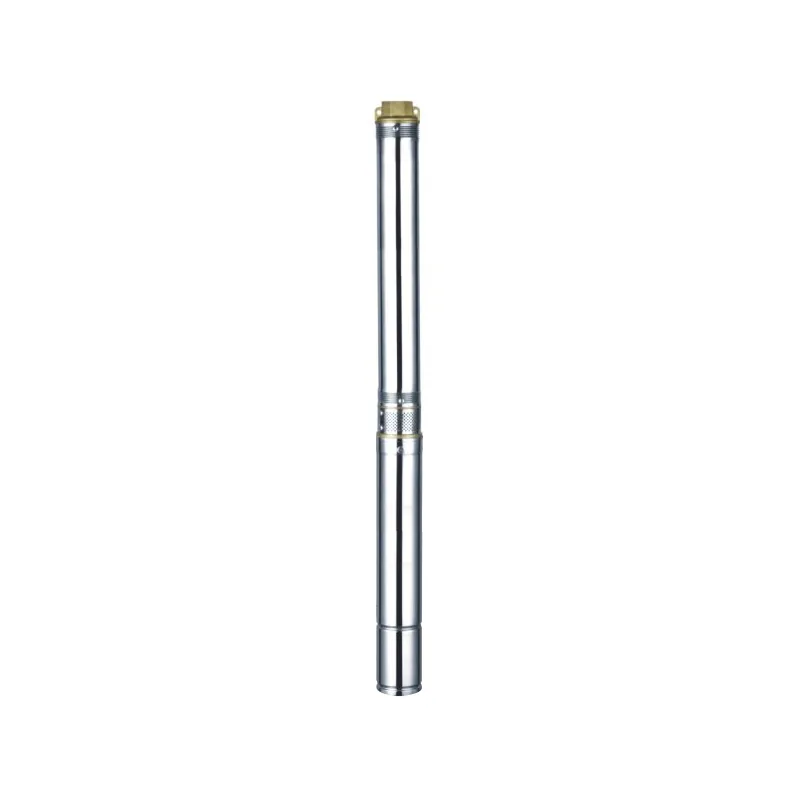
Deep well pumps are a specialized category of submersible water extraction equipment designed to draw groundwater from significant depths, typically ranging from tens to hundreds of feet below the surface. These pumps are engineered for applications requiring reliable access to water in residential, agricultural, industrial, and municipal settings, offering solutions for scenarios where surface water sources are inaccessible or insufficient. Their robust construction and operational efficiency make them indispensable for environments reliant on consistent water supply, such as wells, boreholes, and remote installations.
Applications of deep well pumps are diverse, encompassing potable water supply for households, irrigation for large-scale farming, livestock hydration, and industrial processes requiring consistent water flow. In residential settings, these pumps are critical for ensuring uninterrupted water access in areas with limited municipal connections. Meanwhile, agricultural operations rely on high-capacity models to support crop irrigation and livestock needs, ensuring scalability to match fluctuating demand. Industrial deployments often prioritize pumps with advanced material compositions to withstand corrosive or abrasive water conditions.
Key factors influencing pump selection include well depth, water yield requirements, and operational environment. Shallow wells may accommodate lower-pressure systems, while deeper installations demand robust designs capable of sustaining high lifting capacities over extended periods. Environmental considerations, such as water temperature, abrasives, or chemical composition, further guide pump customization to enhance durability and performance.
In summary, deep well pumps represent a versatile and essential solution for accessing groundwater across various use cases. By distinguishing between submersible and jet mechanisms, and tailoring designs to meet depth, flow, and environmental demands, these pumps ensure efficient and reliable water extraction for diverse operational needs. Their adaptability underscores their critical role in modern infrastructure, supporting agriculture, industry, and daily living in areas dependent on subsurface water resources.
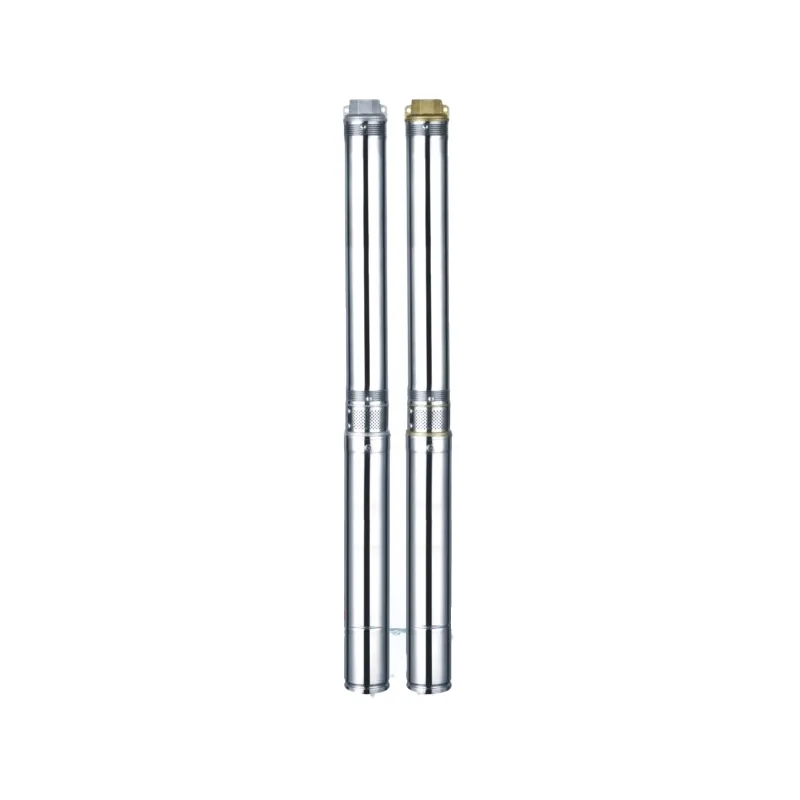
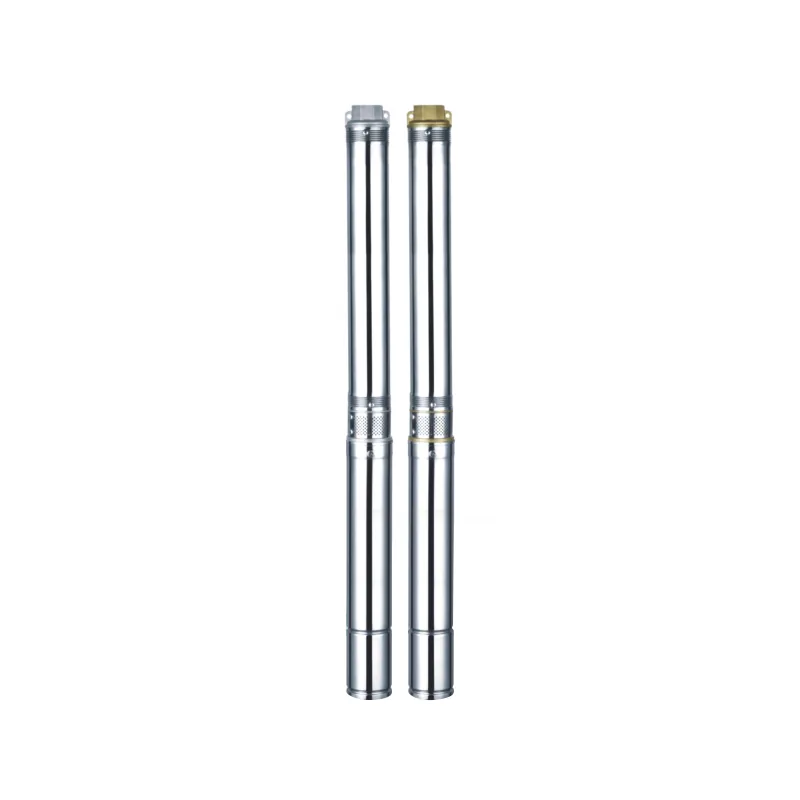
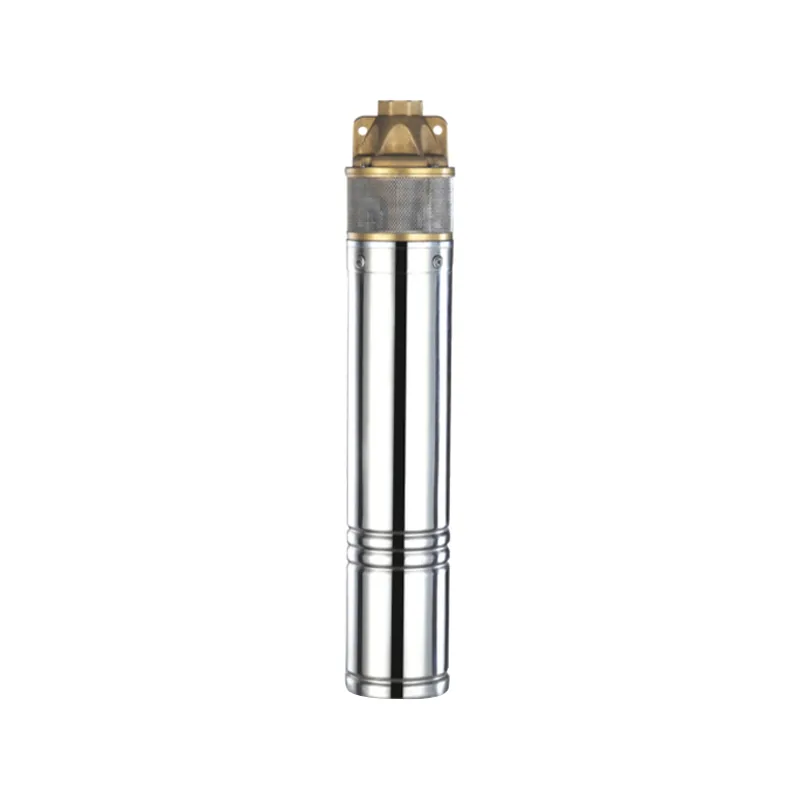
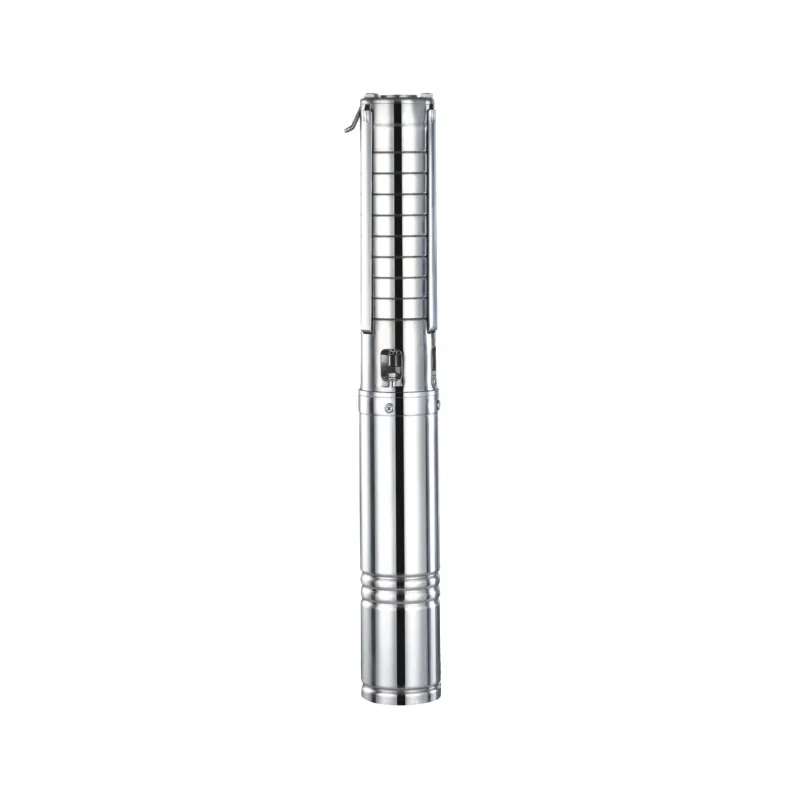
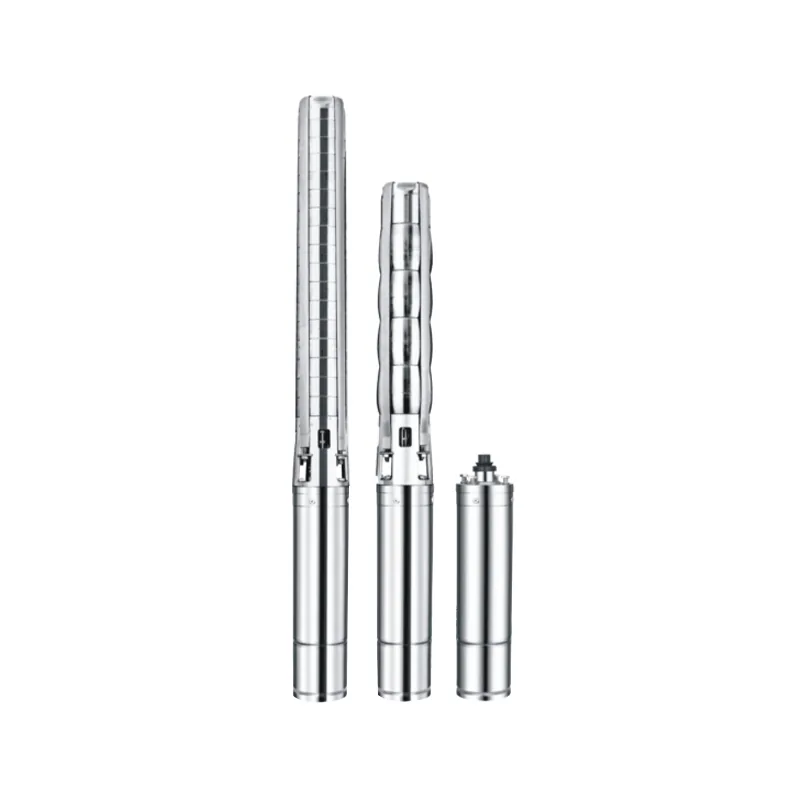
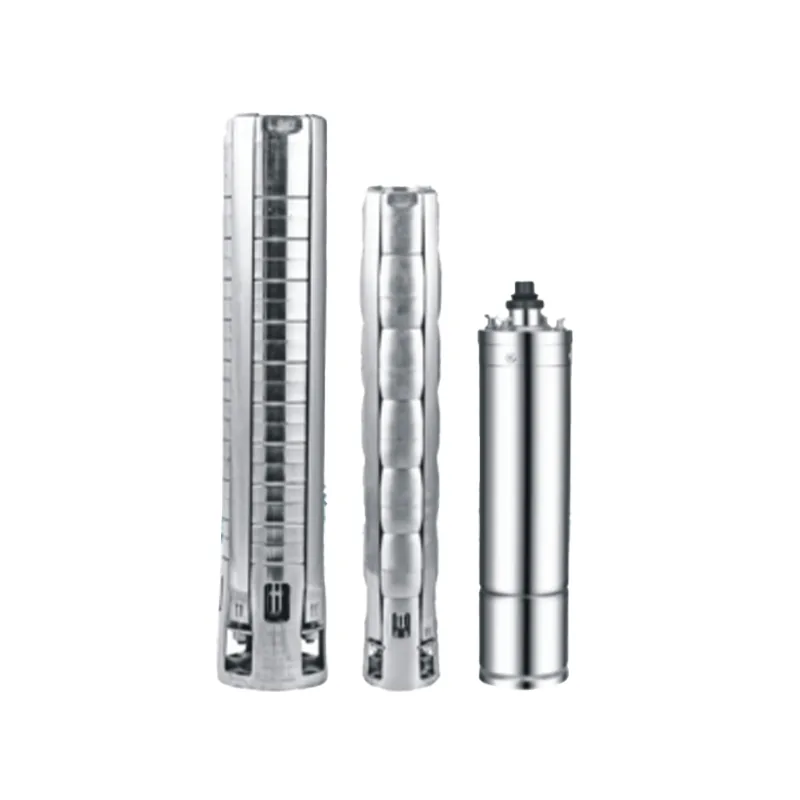
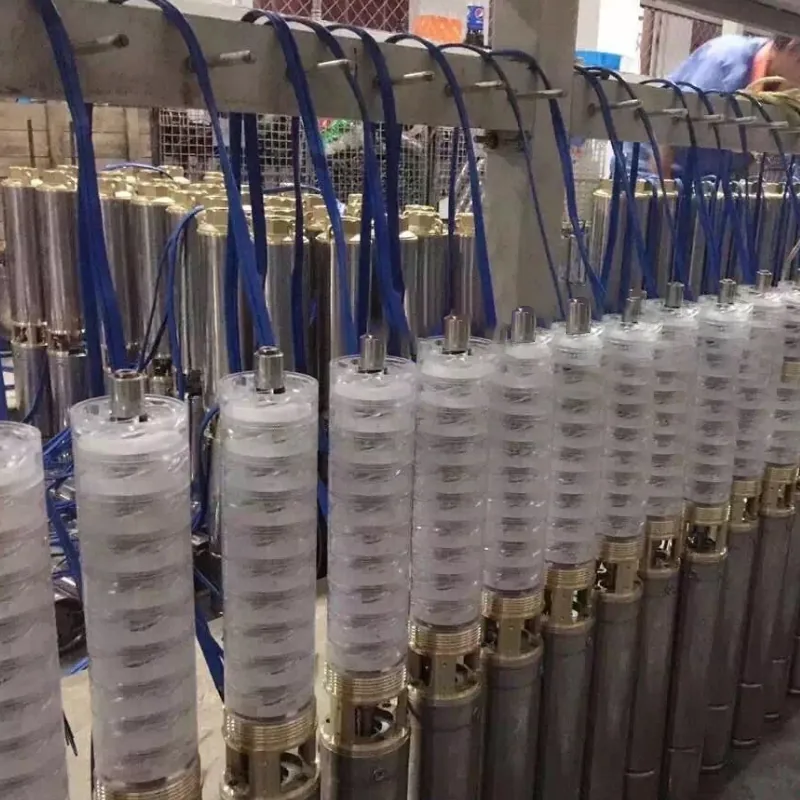
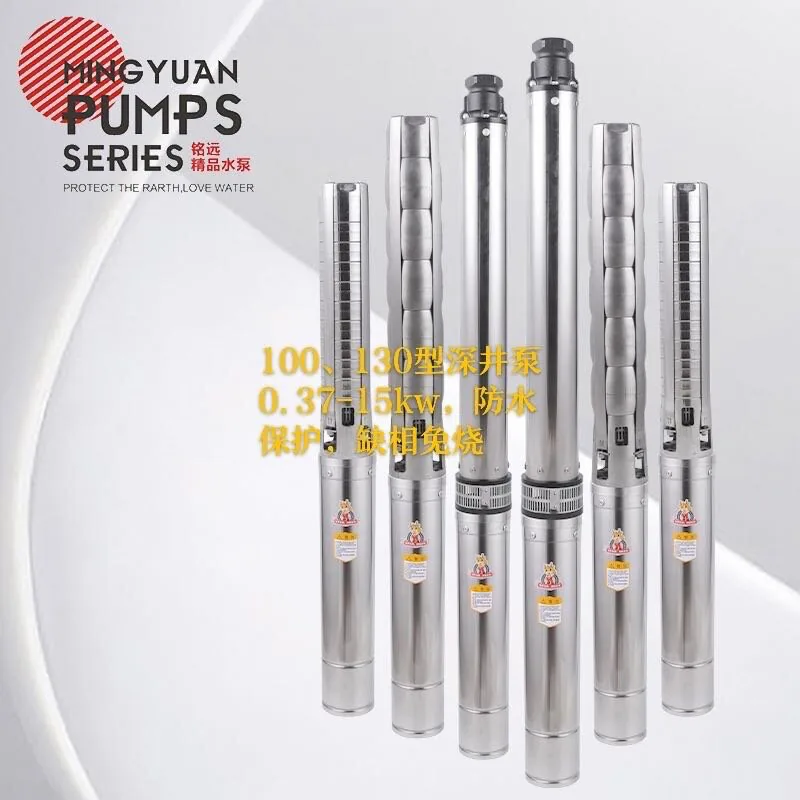
Zhejiang MingYuan Pump Co., Ltd. is located in Liangshan Industrial Zone, Daxi Town, Wenling City, the "hometown of water pumps", close to National Highway 104 and National Highway G15, at the Daxi exit. The company is a professional China Submersible Pump manufacturer and wholesale Submersible Pump factory integrating scientific research, design, production, and sales online. The company has always been committed to innovation in technology and management, and has developed water pumps suitable for industrial and mining enterprises, construction sites, urban water supply, farmland irrigation and drainage, high-rise building water supply, fire protection, industrial water treatment, sewage treatment,t and other industries based on market demand. The company's leading products include: 3SDM, 3.5SDM, 4SDM, YQJD series stainless steel deep well pumps; QGD series screw submersible pumps; QXD, QD series small submersible pumps; QY series oil-immersed submersible pumps; WQD, WQ series sewage and sewage submersible pumps; WQV, WQK series cutting sewage and sewage submersible pumps; WZB, QB, CPM, DTM, JET series land pumps; RG, ISG, SGR, SG series pipeline pumps, etc. The company has successively obtained the national industrial product production license, agricultural machinery promotion license, and obtained IS09001: 2015 quality management system certification.
Founded in
Factory area
Export ratio
Number of employees
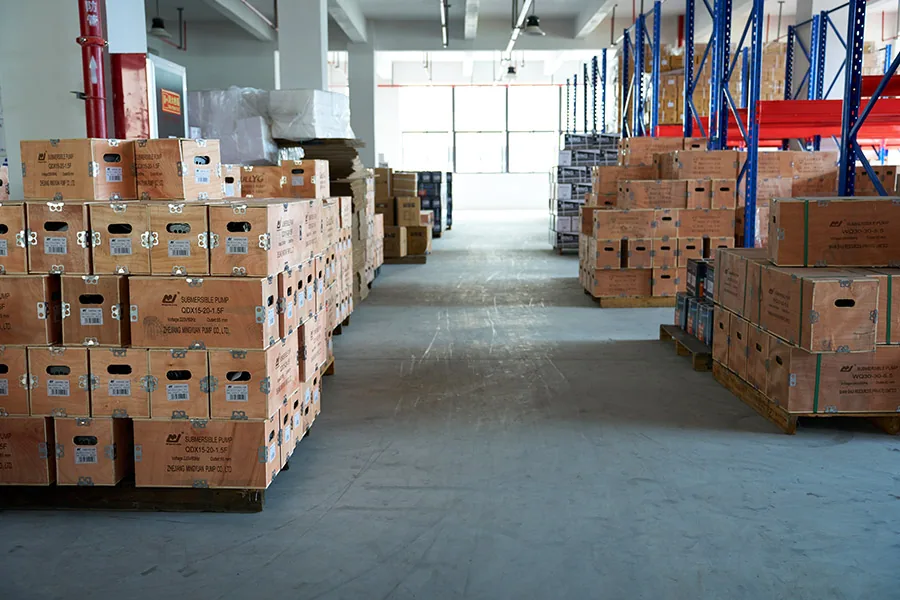
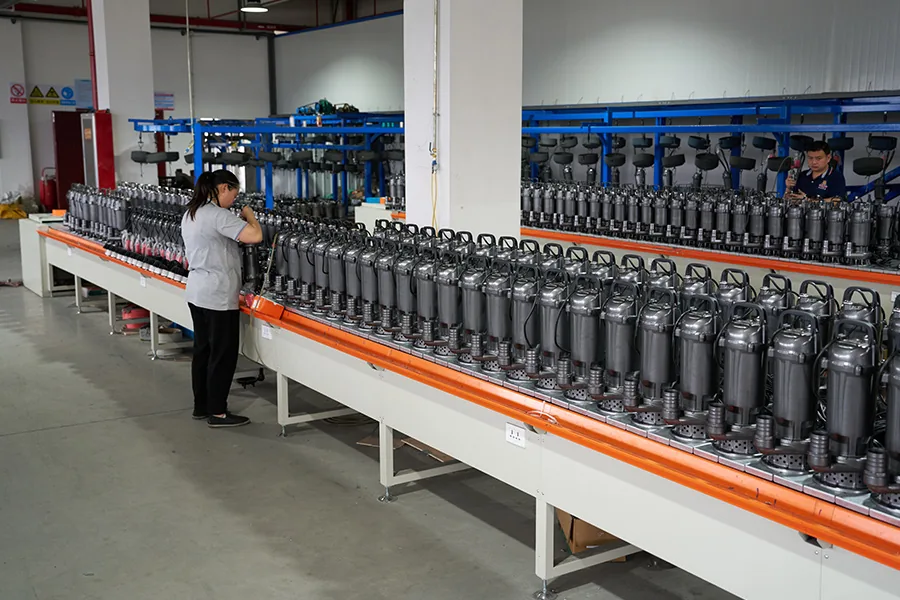
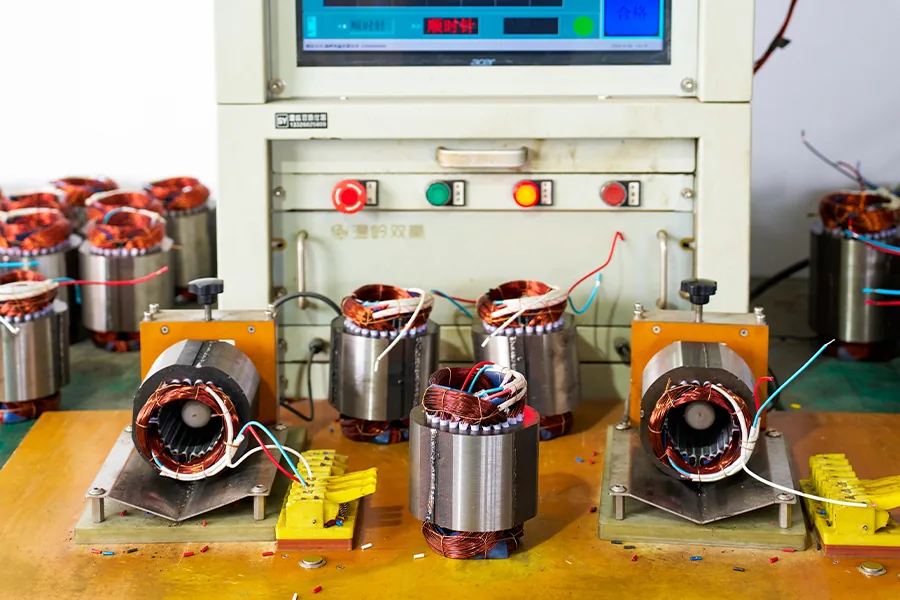
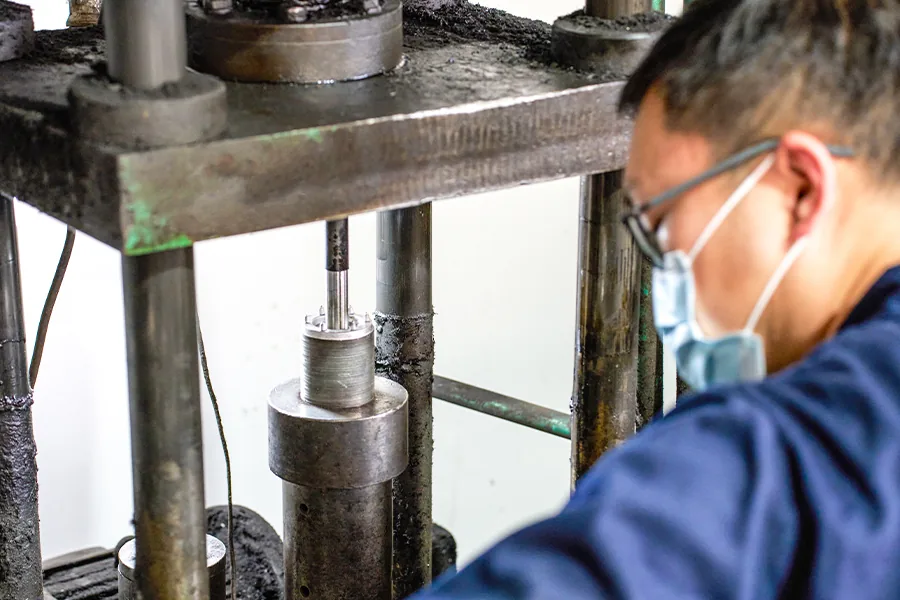
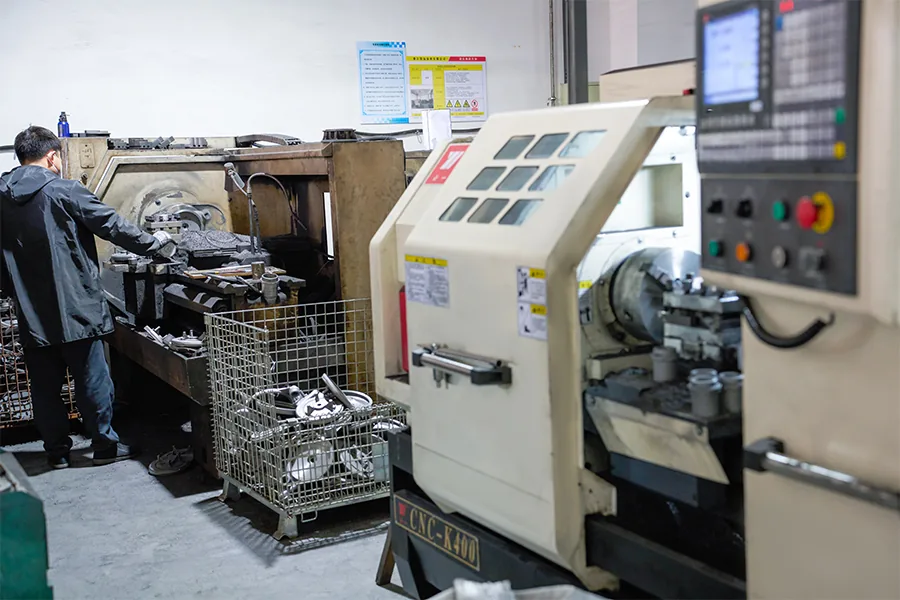
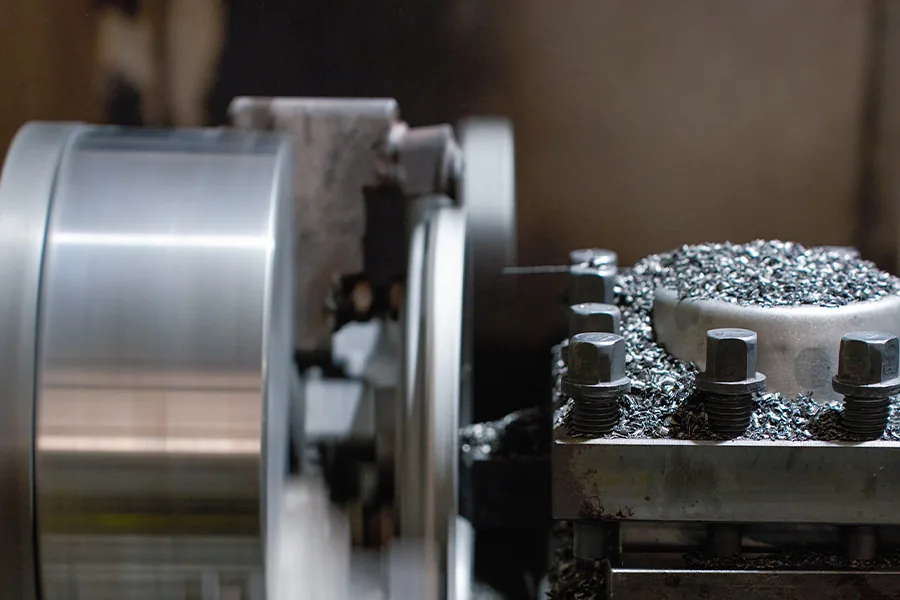
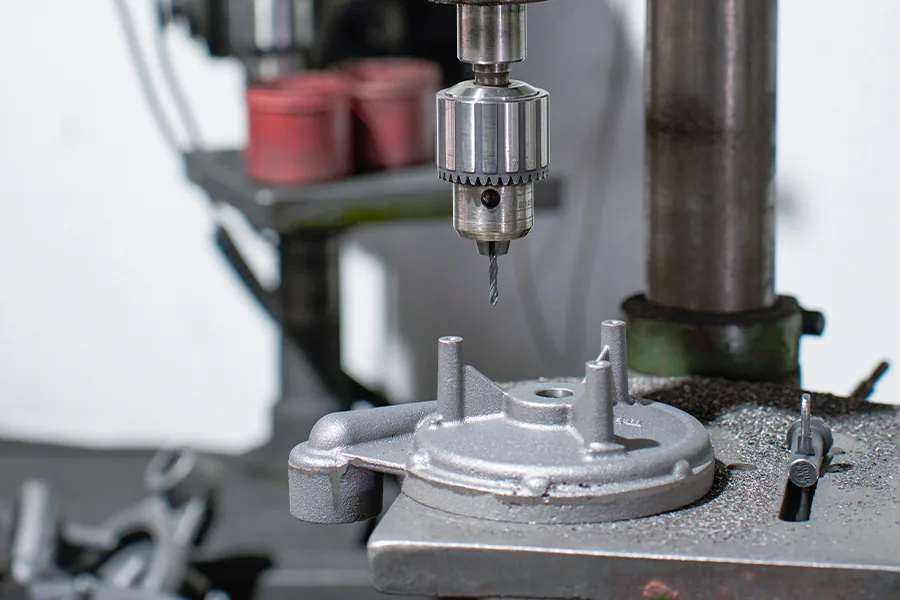
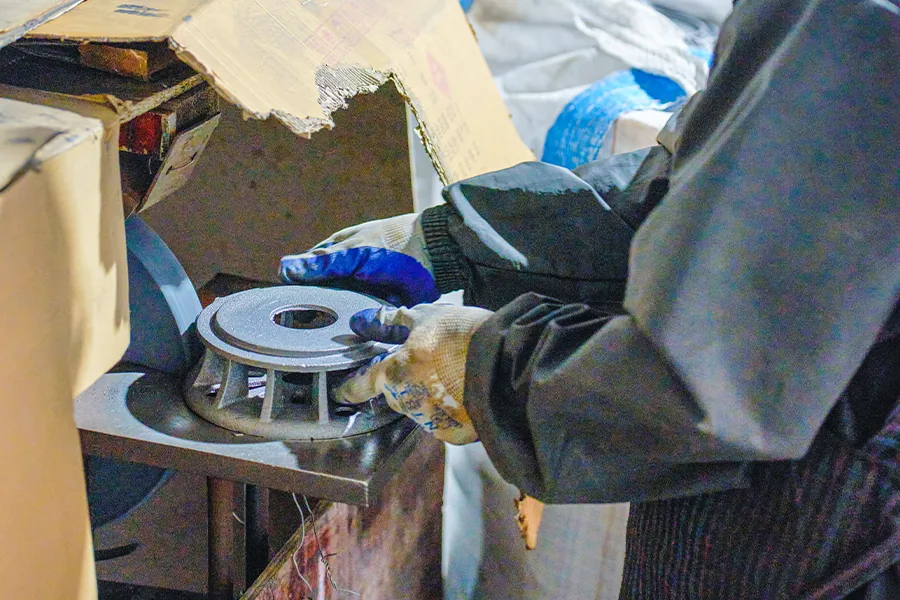
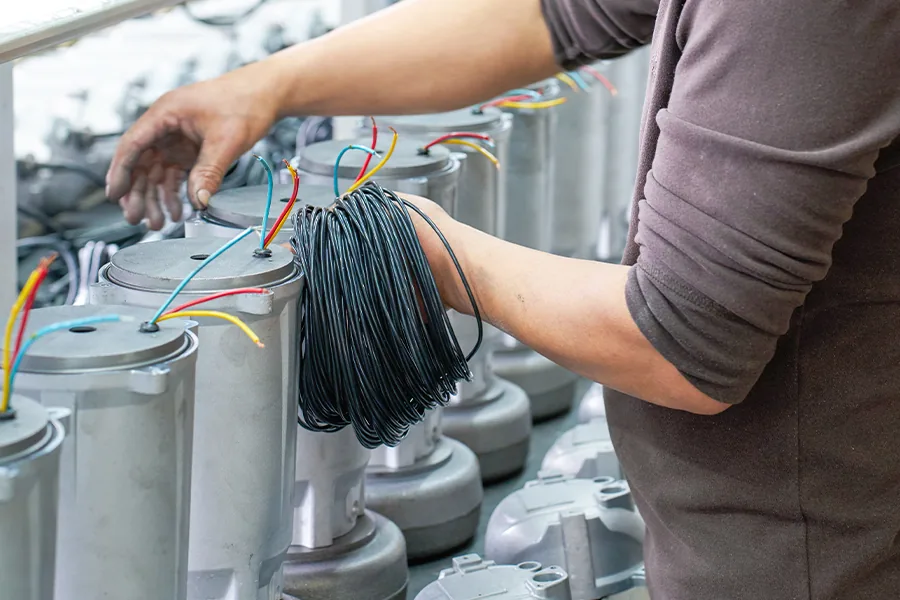
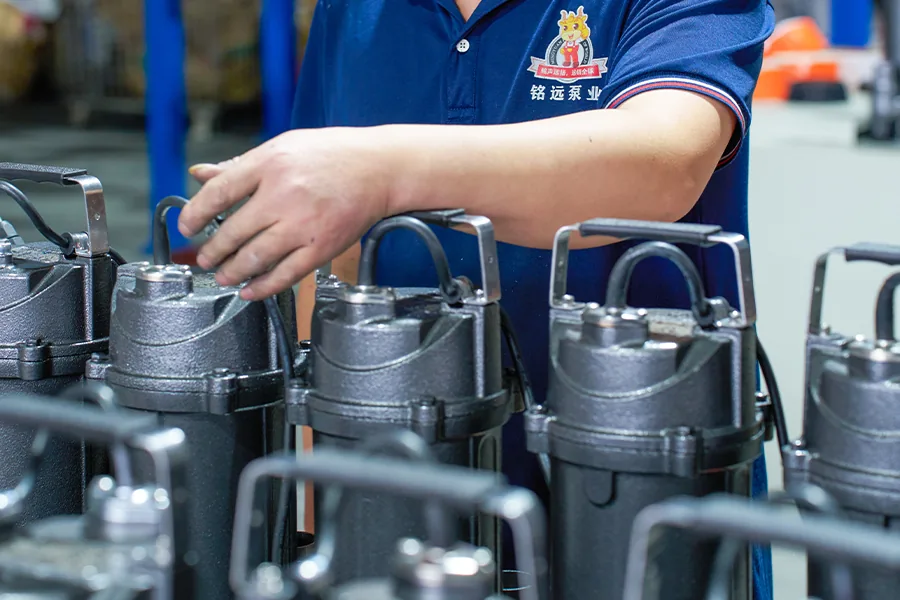
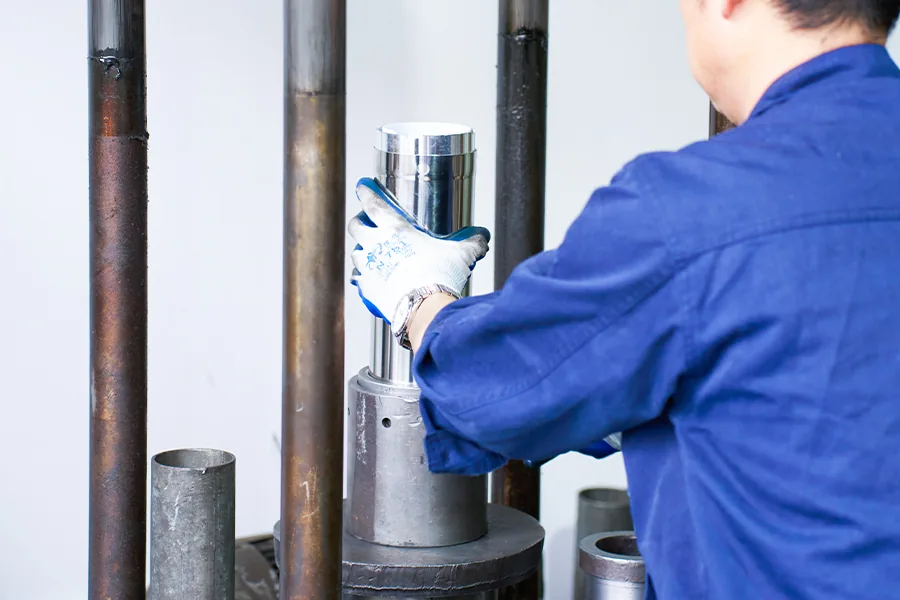
The company continues to upgrade and optimize workshop equipment in order to produce products that satisfy customers.
Wastewater systems in demanding environments require pumps that withstand severe...
View MoreOff-grid water supply solutions increasingly rely on solar energy. Remote irriga...
View MoreSubmerged pumping applications demand equipment that performs flawlessly underwa...
View MoreWastewater systems depend on reliable pumping equipment. Municipal treatment pla...
View MoreWater access defines agriculture and rural living. Irrigation. Livestock. Drinki...
View MoreSewage pumps move dirty water. They handle solids. They run submerged. They work...
View MoreThe submersible pump industry plays a vital role in sectors such as agriculture, construction, sewage treatment, and residential water supply. As demand for efficient and reliable fluid handling systems continues to grow, more users are turning to advanced solutions provided by a high efficiency submersible pump supplier.
A submersible pump is a device designed to operate while fully submerged in the fluid it is intended to move. It typically consists of a sealed electric motor and an impeller system enclosed in a waterproof casing. These pumps are used in applications ranging from draining floodwater and emptying tanks to supplying clean water from wells and handling wastewater in municipal systems.
The compact design and submersion capability of the submersible pump help prevent air-lock issues and allow for efficient vertical lifting of liquids. This makes it suitable for deep well applications, as well as for use in limited-space environments such as basements or narrow boreholes.
A high efficiency submersible pump supplier provides pump solutions that are engineered for reduced energy consumption and stable performance. These suppliers focus on design improvements such as advanced motor technology, precision-balanced impellers, and corrosion-resistant materials to support long-term usage with little power waste.
Choosing a high efficiency submersible pump supplier helps businesses and homeowners lower operating costs over time. These suppliers often offer a wide range of models suited for various flow rates and pressure requirements, enabling customers to select a pump that fits their actual usage conditions.
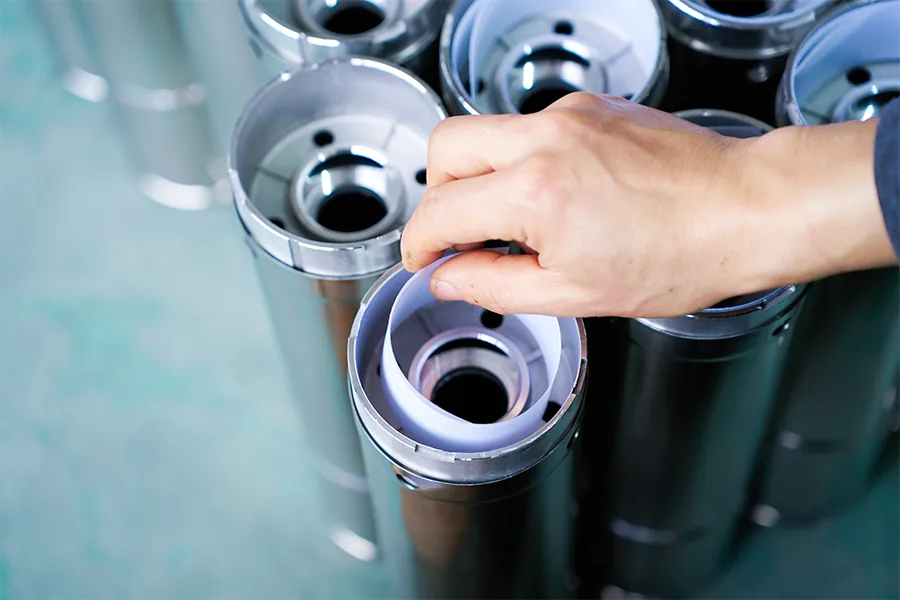
Behind every quality submersible pump is a factory equipped with the tools and systems to carry out material processing, motor assembly, quality inspection, and performance testing. A capable factory can produce a wide range of pump types, including clean water pumps, sewage pumps, and deep well submersibles.
A submersible pump factory typically manages the full manufacturing process—from casting and machining components to assembly and waterproof sealing. Factories that emphasize structured production and testing protocols are better positioned to deliver pumps that meet consistent performance expectations.
Some high efficiency submersible pump suppliers operate their own factories, while others partner closely with certified manufacturers. Either way, the factory's role ensures that each submersible pump is built to required tolerances and can handle demanding environments.
Many factories and suppliers offer submersible pump OEM service, which allows clients to request customized designs and specifications based on their application needs. OEM (Original Equipment Manufacturer) service is commonly used by project contractors, distributors, and private-label brands seeking unique pump features or customized branding.
Through submersible pump OEM service, buyers can specify adjustments in pump housing materials, impeller size, motor wattage, voltage compatibility, and even packaging. This service is particularly useful in large projects where system integration, performance consistency, or local compliance is required.
A high efficiency submersible pump supplier that provides OEM service adds further value by helping customers select pump configurations that reduce energy use while still meeting system goals.
The submersible pump industry combines technical design, factory precision, and application knowledge to provide solutions for a wide range of fluid handling tasks. A reliable high efficiency submersible pump supplier contributes to energy savings, stable operation, and product adaptability—especially when paired with factory support and OEM service. By understanding how these roles function within the industry, buyers can make more informed decisions that support both performance and long-term value.
 English
 Español
 العربية